ES MIG 5183 is designed to provide the highest possible strength in the as-welded condition of alloy AA 5083 and similar high-magnesium alloys.
The more common ES MIG 5356 typi- cally fails to meet the as-welded tensile require- ments of AA 5083.
The alloy is typically used in marine and structural applications where high strength, high fracture toughness for impact resistance and exposure to corrosive elements are important.
The alloy is not recommended for elevated temperature applications due to its susceptibility to stress corrosion cracking. The alloy is non-heat treatable.
ES MIG 5356 is the most widely used welding alloy and can be classified as a general-purpose type filler alloy.
ES MIG 5356 is typically cho- sen because of its relatively high shear strength.
The 5XXX alloy base material, welded with ES MIG 5356, with a weld pool chemistry greater than 3% Mg and service temperatures in excess of 65�°C, is susceptible to stress corrosion cracking.
ES TIG 5356 is the most widely used welding alloy and can be classified as a general-purpose type �ller alloy.
ES TIG 5356 is typically chosen because of its relatively high shear strength.
The 5XXX alloy base material, welded with ES TIG- 5356, with a weld pool chemistry greater than 3% Mg and service temperatures in excess of 65C, is susceptible to stress corrosion crack- ing.
ES TIG 70S-6 is a copper-coated Mn-Si-alloyed W3Si1/ER70S-6 solid rod for the GTAW of non-alloyed steels, as used in general construction, pressure vessel fabrication and shipbuil-ding.
ES TIG 70S-3 is a copper-coated Mn-Si- alloyed W2Si/ER70S-3 solid rod for the GTAW of non-alloyed steels, as used in general construction, pressure vessel fabrication and shipbuil- ding.
Bare, corrosion-resistant, duplex welding rods for welding austenitic-ferritic stainless alloys of the 22% Cr, 5% Ni, 3% Mo types.
ES TIG 2209 has high general corrosion resistance. In media containing chloride and hydro- gen sulphide, the alloy has high resistance to intergranular corrosion, pitting and especially to stress corrosion. The alloy is used in a variety of applications across all industrial segments.
ES MIG 316LSi a continuous, solid , corrosion-resistant, chromium-nickel-molybdenum wire for welding austenitic stainless alloys of the 18% Cr -8% Ni and 18% Cr -10% Ni -3% Mo types.
ES MIG 316LSi has good general corrosion resistance; in particular, the alloy has very good resistance to corrosion in acid and chlorinated environments.
The alloy has a low carbon con- tent which makes it particularly recommended when there is a risk of intergranular corrosion.
The higher silicon content improves the welding properties such as wetting.
The alloy is widely used in the chemical and food processing industries, as well as in shipbuilding and various types of architectural structure.
ES MIG 2209 a continuous, solid, corrosion-resistant, duplex wire for welding austenitic-ferritic stainless alloys of the 22% Cr, 5% Ni, 3% Mo types.
ES MIG 2209 has high general corrosion resistance. In media containing chloride and hydrogen sulphide, the alloy has a high resis- tance to intergranular corrosion, pitting and espe- cially to stress corrosion.
The alloy is used in a variety of applications across all industrial seg- ments.
ES EA2 is a copper-coated, molybdenum-alloyed wire for the submerged arc welding of non-alloyed and low-alloyed steels.
ES EA2 Submerged arc welding wire (SAW) used for joining fine grain steels resistant to high temperatures, structural steels, construction naval vessels, pressure vessels, shipbuilding steels, pipes and pipeline steels up to grade X70, etc.
ES EA2 can be combined with ES FLUX 161, ES FLUX 171 and ES FLUX 181.
ES NiCrFe-3 a nickel-based electrode for welding nickel alloys such as Inconel 600 and similar Inconel alloys, cryogenic steels, martensitic to austenitic steels, dissimilar steels, heat-resistant steels and castings with limited weldability.
High creep resistance up to 815�°C, High resistance to embrittlement, High toughness also at low temperature (-196�°C), High resist-ance to carburization and extra alloyed with ~6% Mn to provide hot cracking resistance.
ES 309L-17 is an over-alloyed, stainless electrode for welding stainless to mild steel and low-alloy steel, for surfacing mild steel and for welding the root runs in clad steel.
The electrode has excellent weldability in all positions except vertical down, on both AC and DC.
Bare, corrosion-resistant, chromium-nickel rods for welding stabilised austenitic chromium-nickel alloys of the 18% Cr-8% Ni type.
The rods are stabilised with niobium, which provides good resistance to the intergranular corro- sion of the weld metal. Due to the niobium content, this alloy is recommended for use at hig- her temperatures.
ES FLUX 161 is designed for the single-wire, multi-run butt welding of mild, medium and high tensile steels with impact strength requirements down to -40C/-60C.
Due to the non-alloying effect, ES FLUX 161 is designed for use with a suitable alloying wire. ES FLUX 161 can be used on DC.
A nickel-based rod alloyed with about 30% Cu, 2% Ti and 1% Fe for the GTAW of base materials of the same type. It can also be used for joining these alloys to steels.
ES TIG NiCu-7 is norm-ally welded with pure Ar as the shielding gas.
Typical applications include heat exchangers, piping, pumps, valves and process vessels in the chemical, offshore and marine industries.
ES EA4 is a manganese-alloyed, copper coa-ted wire for the submerged arc welding of medium- and high-strength structural steels.
ES EA4 should preferably be used together with non-alloying or slightly alloying fuxes, such as ES FLUX 161, when high weld metal quality requirements must be met.
ES EA4 Submerged arc welding wire (SAW) for joining fine grain and high temperature resistant steels, structural steels, steels for shipbuilding, steels for pressure vessels, production of steel pipes up to grade X80, high-strength steels, etc.
ES EA4 can be combined with ES FLUX 161, ES FLUX 171 and ES FLUX 900.
Bare, corrosion-resistant, chromium-nickel welding rod for welding the 24%Cr, 13%Ni alloyed types of steel.
The alloy is also used for welding buffer layers on C/Mn steels and for welding dissi- milar joints. When using the wire for buffer layers and dissimilar joints, it is necessary to control the dilution of the weld.
ES TIG 309L has good general corrosion resistance.
When used for joining dissimilar materials, the corrosion resistance is of secon- dary importance.
ES 11018-G is an LMA electrode dried to a very low moisture content and suitable for the welding of high-strength, low-alloyed steels, at room temperature or with moderate preheating.
Bare, corrosion-resistant, chromium-nickel-man-ganese welding rods for welding austenitic stainless alloys of the 18% Cr, 8% Ni, 7% Mn types. ES TIG 307 has general corrosion resistance similar to that of the corresponding parent metal.
The higher silicon content improves the welding properties such as wetting. When used for joining dissimilar materials, the corrosion resist-ance is of secondary importance.
The alloy is used in a wide range of applications across the industry, such as the joining of austenitic, man- ganese, work-hardenable steels, as well as armour plate and heat-resistant steels.
Bare, corrosion-resistant, chromium-nickel TIG rod. ES TIG 308L has good general corrosion resistance.
The alloy has a low carbon content which makes it particularly recommended when there is a risk of intergranular corrosion.
The alloy is widely used in the chemical and food-processing industries, as well as for pipes, tubes and boilers. Suitable for the joining of stainless steels of the18% Cr-8% Ni type with a low carbon content and Nb-stabilised steels of the same type if the service temperature does not exceed 350C.
It can also be used for welding Cr steels, except in sulphur-rich environments.
ES SG2 is a bare Mn-Si-alloyed G3Si1/ER70S-6 solid wire for the GMAW of non-alloyed steels, as used in general construction, automotive components, pressure vessel fabrica tion and shipbuilding.
ES SG2 taking MAG welding oper-ations to new levels of performance and all-round ef�ciency, especially in robotic and mechanised welding. Characteristic features include excellent start properties; trouble-free feeding at high wire speeds and lengthy feed dis- tances; a very stable arc at high welding currents; extremely low levels of spatter; low fume emission; reduced contact tip wear and improved protection against corrosion of the wire.
ES MIG 80S-Ni1 is a 0.9Ni-alloyed (ER80S-Ni1), copper-coated, solid wire for the GMAW of low-temperature, ne-grained steels.
The wire provides good impact toughness down to -50C and is especially suitable for use in the construction of offshore platforms, pressure vessels, and pipelines.
ES TIG 90S-G is a 2.5Cr-1.0Mo-alloyed, copper-coated rod for the GTAW of creep-resistant steels such as pipes in pressure vessels and boilers of similar composition, Steam Genera-ting Power Plant with service temperatures of up to 600C, but it is also suitable for welding high strength steels.
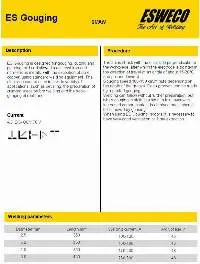
ES Gouging is designed for gouging, cutting and piercing mild and alloyed steel, cast iron and non-ferrous metals, with the exception of pure copper, using standard welding equipment.
The electrode can be used in a wide variety of applications, such as beveling, the preparation of cracked areas before welding and the back-gouging of root runs.
ES TIG 80S-Ni2 is 2.4Ni-alloyed (ER80S-Ni2), copper-coated rod for the GTAW of low-temperature, �ne-grained steels in applications such as pressure vessels, pipes and the offshore indus- try, with a minimum yield strength of up to 470 MPa. The wire provides good impact toughness down to -60C.
ES 309MoL-17 is an over-alloyed, stainless-steel electrode for use as a buffer layer when welding acid-resistant clad steels and stainless steels to other types of steel.
ES 309MoL-17 has outstanding welding properties on both AC and DC.
The electrode can be used in all positions apart from vertical down
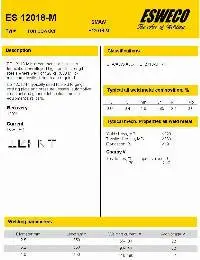
ES 12018-M is recommended for use in fabrication low alloyed high tensile strength steels where weld of 120 ksi (830 MPa) minimum tensile strength are required.
ES 12018-M typically used to weld forging, casting plate and pressure vessels, automotive industrial and general fabrication, mobile equipment's railcars.
ES 10018-M used for welding high strength low alloy steels in the 100,000 psi tensile strength range.
It is ideal for conditions of high heat and humidity due to the moisture resistant coating which helps prevent hydrogen cracking and starting porosity.
ES 10018-M is an excellent choice for reinforcing steels and high tensile steels.
ES SG3 is a bare Mn-Si-alloyed G4Si1/ER70S-6 solid wire for the GMAW of non-alloyed steels, as used in general construction, automotive components, pressure vessel fabrica tion and shipbuilding.
It has a slightly higher manganese and silicon content than ES SG2 to increase the weld metal strength.
This also promotes a low sensitivity to surface impurities and contributes to smooth, sound welds.
ES SG3 taking MAG welding operations to new levels of performance and all-round ef�ciency, especially in robotic and mechanised welding.
Characteristic features include excellent start properties; trouble-free feeding at high wire speeds and lengthy feed distances; a very stable arc at high welding currents; extremely low levels of spatter; low fume emission; reduced contact tip wear and improved protection against corro- sion of the wire.
ES TIG 80S-B8 is a 9Cr-1Mo-alloyed, copper-coated rod for the GTAW of high temperature steels and steels for hot hydrogen service,especially in oil refineries.
ES TIG 80S-B8 typically used in chemical industries for heat exchangers, boilers, piping, ammonia synthesis process and pressure vessels at service temperatures up to 1100F (590 C).
ES NiCrFe-2 is a nickel-based electrode for welding Inconel 600 and similar alloys, cryogenic steels (e.g. 9Ni and 5Ni steels), martensitic to austenitic steels, dissimilar steels, heat-resistant steel castings with limited weldability and so on.
The weldability is good in all positions, even in the over-head position.
Used extensively in the furnace equipment & repair / petro-chemical industries.
ES TIG 90S-B3 is a 2.5Cr-1.1Mo-alloyed (ER90S-B3), copper-coated rod for the GTAW of creep-resistant steels like SA-387 Grade 22, A335 Grade P22 or similar materials.
ES TIG 90S-B3 typically used in chemical industries for heat exchangers, boilers, piping and pressure vessels at service temperatures up to 1100F (590 C)
Bare, corrosion-resistant, chromium-nickel welding rods for welding materials of the 29% Cr, 9% Ni types.
ES TIG 312 has good oxidation resistance at high temperatures due to its high content of Cr.
The alloy is widely used for joining dissimilar steels, especially if one of the components is fully austenitc, and for steels that are dificult to weld, i.e. machine components, tools and austenitic-manganese steels.
A nickel-based, corrosion- and heat-resistant, 22% Cr, 9% Mo, 3.5% Nb rod for the GTAW of high-alloyed steel, heat-resistant steel, corrosion-resistant steel, 9% Ni steels and similar steel with high notch toughness at low tempera- tures.
It is also suitable for joining dissimilar metals of the types mentioned above.
ES TIG NiCrMo-3 is normally welded with pure Ar as the shielding gas.
A nickel-based, corrosion- and heat-resistant, 20% Cr, 3% Mn, 2.5% Nb rod for the GTAW of high-alloyed steel, heat-resistant steel, corro-sion-resistant steel, 9% Ni steels and similar steels with high notch toughness at low temperatures.
It is also suitable for joining dissimilar metals of the types mentioned above.
ES TIG NiCr-3 is usually welded with pure Ar as the shielding gas.
A nickel-cored electrode for welding normal grades of cast iron.
The weld metal is soft and easily machinable. Deposition is performed on cold or slightly preheated material.
The electrode is suitable for joining cast iron for the recti�cation of casting and the repair of broken parts.
ES Ni-Cl is specifically suited for repairing cracked or porous castings and to weld cast iron to itself or dissimilar metals such as low alloy and carbon steels.
ES 8018-G is a NiCu-alloyed LMA electrode, which deposits a weld metal with good corrosion resistance to sea-water and ï¬?ue gases, for the welding of weatherproof steel and for shipâ??s hull structural steel.
The weld metal has excellent mechanical properties.
It is particularly suitable for welding the shell plating of ice-breakers and other ships, which work under conditions where the protective paint coating wears off.
86 Aluminium Alloy Suppliers
Short on time? Let Aluminium Alloy sellers contact you.